How to Choose a Carton Counting System for Your Factory
The right carton counting system is the one that can reliably distinguish the units your factory needs to deliver, at the point where those units can be controlled. A counter rated for the folder gluer’s maximum speed is not enough if overlapping blanks, rejected cartons, manual removals, or bundle transfers make the recorded quantity different from the quantity shipped.
Selection therefore starts with the production path rather than a sensor specification. Define what constitutes a carton, where the count becomes authoritative, and how the system will handle rejects, order changes, and interruptions. Then compare technologies against the actual carton range, available installation space, control interfaces, and required acceptance performance.
Decide what the count needs to represent
A carton factory can have several legitimate counts for the same order: sheets fed, cartons produced, cartons rejected, cartons placed in bundles, and cartons accepted for shipment. These numbers should not be treated as interchangeable. A counter at the feeder, for example, cannot on its own confirm that every sheet became an acceptable finished carton.
Before requesting quotations, identify the decision the count will support. A machine-output figure may be sufficient for monitoring productivity. An order-fulfillment count needs a defined relationship to rejects, samples, rework, and cartons removed by operators. If bundles or pallets are counted instead of individual cartons, the control system also needs a reliable way to confirm the quantity in each bundle.
Agree on the unit of measurement in writing. A flat folding carton, a glued corrugated box blank, a nested product, and a completed bundle present different detection problems. Specify whether the system must count individual items, create predetermined batches, verify an existing batch, or perform a combination of these functions.
Placement follows from that decision. A counting point after folding and gluing may be closer to finished output, but access can be constrained by shingled flow or downstream equipment. A point before inspection may provide a clean signal but requires rejected pieces to be deducted accurately. A second verification point can help reconcile counts, although it adds equipment, integration work, and another measurement whose limitations must be understood.
Match the detection method to the carton flow
There is no universally best counting technology. The suitable method depends on whether cartons pass one at a time, overlap, travel in stacks, or form bundles. Ask suppliers to explain how their system identifies one unit and what happens when that assumption fails.
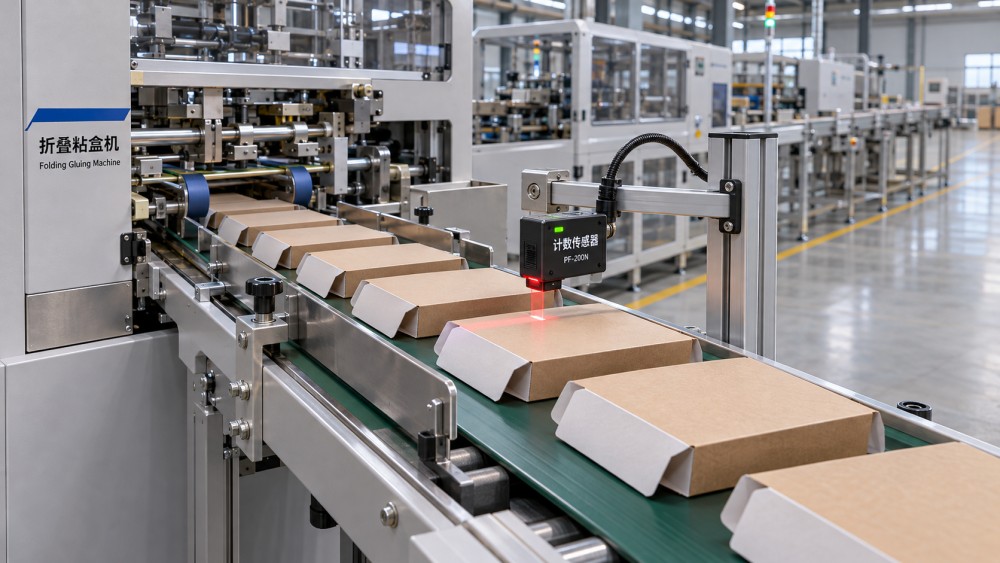
On a folder gluer delivery, cartons may leave as an overlapping stream. A simple beam interruption might identify the front of the stream rather than every individual piece. The supplier should show how individual carton edges are resolved at the intended overlap, including when speed changes or the stream becomes uneven.
Carton characteristics matter as much as nominal dimensions. Prepare samples covering the smallest and largest formats, thin and thick board, dark or reflective printing, cutouts, irregular edges, and products that tend to curl. A system that performs well on a plain rectangular sample may need different positioning or settings for a windowed carton or a corrugated blank with a complex profile.
Also distinguish a device’s rated response speed from its usable line speed. Detection depends on the smallest separation or visible edge at the sensor, not just cartons per hour. For a shingled stream, the distance between exposed edges can be much smaller than the carton length. The supplier should demonstrate performance at the intended speed and overlap, with enough margin for normal variation rather than only a stable demonstration run.
Plan the line interface before choosing the hardware
A counting system can generate an accurate signal and still fail as a project if it cannot operate the surrounding equipment as intended. Map the interfaces between the counter, folder gluer, conveyor, batch separator, stacker, inspection system, and any palletizing equipment. Identify which machine owns each command and what each machine does if a signal is late, missing, or duplicated.
For batch formation, establish how the counter requests a separation and where the physical separation occurs. Cartons continue moving between detection and separation, so the control logic must account for the product in transit. The required offset can change with speed, product spacing, and conveyor configuration. A batch count that is correct at one speed should be checked during acceleration, deceleration, and stop-and-restart conditions.
Reject handling deserves a separate signal review. If inspection rejects a carton downstream of the counting point, determine whether the reject is physically removed and whether its quantity is deducted from the correct order or bundle. A reject command is not necessarily proof of successful removal. Where quantity assurance depends on removal, consider how the reject event is confirmed and how failed or uncertain events are handled.
Document the control interface in practical terms: available inputs and outputs, communication protocols, signal timing, machine interlocks, and responsibility for programming. If production data will be sent to a manufacturing or order-management system, specify the job identifier, count definitions, timestamps, update frequency, and behavior during a network interruption. Confirm whether data are buffered locally, how they are retransmitted, and how duplicate records are avoided.
Physical integration is equally important. Check mounting space, sensor visibility, guarding, cable routes, lighting requirements, cleaning access, and the ability to adjust for different carton formats. A sensor mounted in a convenient spare space is not useful if operators must remove it to clear a jam or cannot see its target during setup.
Specify how the system handles exceptions
Counting errors do not occur only during steady production. The project specification should describe the expected behavior when cartons back up, a bundle is removed manually, a sensor is obscured, or the line stops with product between the counting and batching points.
Define whether an interruption pauses the active batch, resets it, or requires operator confirmation. Establish who may amend a count, what information is recorded when an adjustment is made, and how partially completed bundles are identified. If the counter loses power, the recovery procedure should prevent an unverified quantity from silently being treated as a complete bundle.
Order changeover also needs an explicit boundary. A new job should not inherit the previous job’s target or count, and cartons already in transit should not be attributed to the wrong order. Where multiple product recipes are used, specify which settings are recalled automatically and which require physical adjustment or operator verification.
Alarms should support action rather than merely report a fault. Agree on the conditions that stop the line, those that generate a warning, and those that mark output for inspection. A system that continues producing during a detection fault needs a clear procedure for isolating and recounting affected cartons.
Compare suppliers using a defined production test
A quotation should be evaluated against a shared test plan, not only against a stated counting accuracy. Ask each supplier to identify the products and conditions covered by its performance commitment, the measurement method, and exclusions. Accuracy is meaningful only when both parties agree on the reference count and the point in the process being measured.
The test plan should include representative carton types and the operating conditions that challenge detection: intended production speeds, normal speed changes, overlap variation, short and long runs, and relevant print or board differences. Include starts, stops, batch changes, and controlled reject events if those functions are part of the scope. A practical reference count may require independently verified quantities; agree on how discrepancies will be resolved before the test starts.
Measure more than the total for a long run. A correct final total can conceal one overcount and one undercount, while individual bundles remain wrong. Where bundle accuracy matters, compare the actual quantity in each sampled or tested bundle with its target. Record false counts, missed counts, uncertain events, recovery actions, and any adjustments needed to keep the system running.
Acceptance criteria should distinguish factory acceptance, if performed at the supplier’s site, from site acceptance on the installed line. A supplier demonstration can show the detection principle, but it may not reproduce the factory’s conveyor geometry, vibration, dust, product handling, or control interfaces. Define the samples, duration, operating range, permitted interventions, and pass criteria for each stage in the contract.
Calculate the full implementation cost
The purchase price of the counter is only one part of the decision. Include brackets and mechanical modifications, electrical work, control programming, safety review, integration with existing equipment, commissioning, training, spare parts, and planned production downtime. If multiple lines are involved, check whether sensors, software licenses, network interfaces, and engineering work are priced per line or shared.
Operating costs depend on the chosen method and the site’s conditions. Optical devices need accessible cleaning and alignment; camera systems may require lighting maintenance and recipe management. Confirm which parts can be replaced by site personnel, what diagnostic information is available, and whether support depends on remote access or specialist visits. Ask how software updates, backups, and replacement hardware will be managed over the equipment’s life.
Estimate benefits using a baseline that the factory can measure: time spent on manual counting, recounts caused by uncertainty, bundle corrections, and disruptions associated with quantity disputes. Do not assume that all manual checks disappear. A system may reduce routine checks while still requiring verification after alarms, product changes, or maintenance. Compare savings with the complete installed cost and the remaining work, rather than with the equipment price alone.
The strongest selection is not necessarily the system with the most features. It is the one whose counting principle fits the carton flow, whose exceptions can be controlled, and whose performance can be demonstrated at the required production point. If those conditions cannot be established for every line, a staged installation on a representative line can expose integration and operating issues before the same design is repeated elsewhere.
Related News
 When Is a Servo Folder Gluer Line Worth the Investment?Is a servo folder gluer line worth the investment? Explore the production challenges, ROI factors, and supplier questions that can guide your decision.Ms. Vivienne Cross
 US Justice Department Investigates Pricing by Major Corrugated Packaging ProducersThe US Justice Department is investigating containerboard pricing by major corrugated packaging producers. Explore potential implications for buyers and supply chains.Ms. Vivienne Cross
 What Affects Folder Gluer Machine Price and Total Cost?Folder gluer machine price is only part of the investment. Discover what drives costs and how to compare quotes, operating expenses, and long-term value.Ms. Vivienne Cross
 How Roll Handling Equipment Price Affects Project ROIRoll handling equipment price affects more than upfront costs. Learn how to compare installed costs, quantify savings, and build a stronger project ROI case.Ms. Vivienne Cross
 How Stacking Machines Reduce Bottlenecks in Sheet PlantsStacking Machines reduce sheet plant bottlenecks by improving pile quality and flow. Discover how to choose and integrate the right system.Ms. Vivienne Cross
 Italian Packaging Machinery Sales Up Just 0.9% as Orders Fall 4.7%Italian packaging machinery sales rose just 0.9% as orders fell 4.7%. Explore UCIMA's figures and what weaker demand could mean for buyers and exporters.Ms. Vivienne Cross