How to Diagnose Sleeve Runout in Flexo Before It Causes Register Drift
Register drift that appears only after a flexographic press reaches production speed is often blamed on the register control system, plate mounting, ink viscosity, or web tension. Those factors matter, but they do not explain every defect that repeats once per sleeve revolution or becomes worse with speed. Sleeve runout is a mechanical source that can create a moving print reference: the plate cylinder surface does not rotate on a true axis, so the print impression and circumferential position change slightly during each revolution.
The practical consequence is not always an immediately visible “out-of-round” print. A press may hold acceptable register during setup, then show intermittent color-to-color movement, repeating halo, fluctuating impression, or a correction system that continuously hunts without reaching a stable position. By the time the defect is obvious, waste and troubleshooting time have already accumulated. The useful diagnostic question is therefore not simply whether a sleeve has runout, but whether the measured movement is sufficient, repeatable, and phase-related to explain the register behavior.
Separate sleeve runout from other register faults
Runout is often used loosely to describe any rotating error. For diagnosis, it helps to separate three conditions:
- Radial runout is variation in the distance from the rotating axis to the sleeve surface. It changes the effective printing radius and can alter impression, dot gain, and the tangential speed at the print nip.
- Axial runout, sometimes described as face wobble, is side-to-side movement of a reference face during rotation. It can affect lateral register and create inconsistent contact across the print width.
- Eccentricity means the sleeve or its mounting reference is not concentric with the true rotation axis. It is a common underlying cause of radial runout, although a dial indicator records the resulting total indicated runout (TIR), not the cause by itself.
A sleeve-related fault normally has a repeatable angular signature. If a visible defect or register correction recurs at the same point of a cylinder revolution, mechanical rotation should be investigated before adjusting process settings. By contrast, register movement that follows splice passage, moisture variation, tension changes, gear disturbances, or intermittent web slip will not reliably stay locked to the sleeve’s angular position.
It is also important to distinguish a stable register offset from drift. A stable offset can often be corrected by normal register adjustment. Drift means the required correction changes while the job runs. If the press controller keeps adding and removing correction at a repeating frequency, an unstable rotating reference, including sleeve runout, becomes a credible suspect.
Read the defect pattern before removing components
The print pattern provides the first direction, especially when production conditions make immediate disassembly impractical. Mark a safe, non-printing reference position on the sleeve, adapter, or cylinder end where permitted by plant procedure. Compare that position with the recurrence of the defect. A mark that aligns repeatedly with the strongest register error is more useful than a general statement that “the print moves at speed.”
Common symptoms that justify a runout check include:
- one color showing a cyclic advance and retard relative to the others;
- a repeating light-dark impression band or periodic dot growth in one unit;
- register that is acceptable at low speed but oscillates as speed increases;
- one sleeve producing a problem while another sleeve on the same station does not;
- anilox-to-plate or plate-to-substrate contact that changes at the same rotational point;
- unexplained changes after a sleeve change, wash-up, crash, or handling event.
These symptoms are not proof. A damaged plate, uneven mounting tape, sleeve swelling, an anilox issue, or a cylinder bearing fault can produce related visual effects. The value of pattern recognition is that it tells the maintenance team where to establish a measurement chain.
Measure the complete rotating stack, not only the sleeve
A common diagnostic error is to remove a suspect sleeve, place it on a bench fixture, find a low reading, and declare the sleeve serviceable. That result may be accurate but incomplete. On press, the effective rotating system includes the drive-side and operator-side support condition, cylinder journals or bearings, air mandrel or adapter, sleeve bore, sleeve body, plate mounting build-up, and sometimes the plate itself. A defect at any interface can appear as sleeve runout at the printing surface.
Before mounting an indicator, make the press safe under the site’s isolation and stored-energy procedures. Pneumatic sleeve systems deserve particular attention: residual air pressure, unintended rotation, and sleeve release hazards must be controlled before hands or measuring equipment are placed near the cylinder.
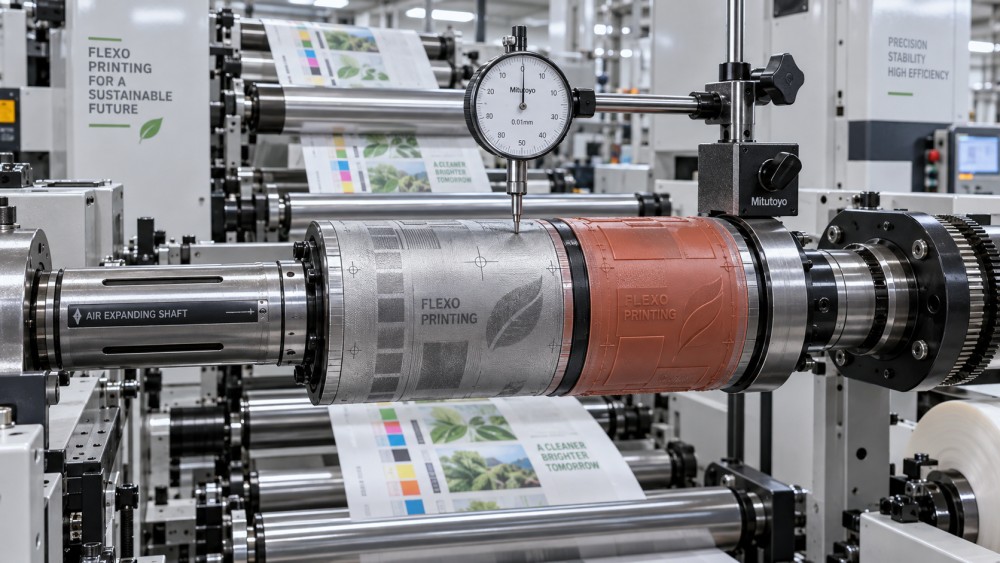
Use a rigid magnetic base or a fixed machine reference that cannot move with the component being measured. A flexible bracket can create its own apparent runout. The indicator tip should contact a clean, undamaged surface at a reasonably perpendicular angle. A poor contact angle, a tip riding on a seam, or dirt under the measuring point can introduce false variation.
The measurement sequence should move from the machine reference outward:
- Check accessible journal or cylinder reference surfaces, where the machine design permits it.
- Measure the bare mandrel, air cylinder, or adapter surface.
- Install the sleeve correctly and measure the sleeve’s outside diameter at several axial positions.
- Check a sleeve end face or other approved axial reference for face movement.
- If the fault remains unexplained, measure the mounted plate surface and inspect the plate/tape build-up.
Rotate slowly by hand through a full revolution, recording the high and low indicator readings and the angular position of the high point. TIR is the difference between those readings. Repeat the check after removing and reinstalling the sleeve. A reading that changes substantially after reinstallation points toward contamination, incomplete seating, air-system behavior, or handling rather than a fixed sleeve geometry problem.
Do not rely on one measurement location. A sleeve with a conical, distorted, or locally damaged body can show different radial readings near each end and at the center. Measuring at several axial stations also helps distinguish a general concentricity problem from a local dent or a sleeve that has been distorted by clamping, storage, cleaning, or impact.
What the measurement pattern reveals
A dial indicator gives more diagnostic value when the waveform is interpreted rather than reduced to a single number. A smooth, single high point once per revolution suggests simple eccentricity: the rotating surface is offset from the true axis. If the high point remains at the same angular position when the sleeve is removed and reinstalled, the sleeve body itself becomes more suspect. If the high point moves relative to the sleeve mark after reinstallation, examine the mounting interface first.
Multiple peaks per revolution can indicate local damage, debris, wear patterns, distortion in an adapter, or a component with more complex geometry error. A sharp spike is often caused by a dent, raised contamination, damaged sleeve edge, plate seam, or indicator contact issue. A broad gradual variation is more consistent with a concentricity or support problem.
Compare the phase of measurements made at different points:
- Bare mandrel and installed sleeve high points align: the source is likely upstream of the sleeve, such as the mandrel, cylinder support, bearing condition, or drive-side structure.
- Bare mandrel is stable but the installed sleeve shows runout: inspect the sleeve bore, internal surface, sleeve body, air expansion behavior, and seating condition.
- Sleeve surface is stable but the plate surface varies: investigate mounting tape thickness, tape overlap, plate distortion, adhesive debris, plate seam condition, or incorrect mounting procedure.
- Radial runout is low but axial movement is high: inspect sleeve end-face seating, axial location features, thrust control, bearing play, and side-load conditions.
Machine documentation should define the allowable TIR for each cylinder, sleeve type, print repeat, and measurement location. It is not good practice to apply one generic tolerance across all flexographic presses. A value that appears small on an indicator can still matter in fine-screen, close-register work, while a larger value may have little visible effect on a less demanding job. The decision should connect the measured condition with the print specification, defect phase, press speed, and OEM acceptance criteria.
Check seating and air support before condemning the sleeve
On air mandrel systems, insufficient, uneven, or leaking air can prevent the sleeve from expanding and seating uniformly. A sleeve may appear locked in place yet remain slightly tilted or supported unevenly. Verify the air supply condition specified by the machine manufacturer, inspect hoses and seals for leakage, and confirm that air ports are not blocked by ink, wash chemicals, tape fragments, or dried contamination.
Cleanliness matters at both the bore and mandrel surface. A thin ink film, dried coating, paper dust mixed with lubricant, or a raised burr can create measurable eccentricity. Aggressive scraping should be avoided because it can damage the reference surface that must remain concentric. Use approved cleaning methods, inspect under good light, and address burrs only according to the equipment supplier’s repair guidance.
Sleeve insertion technique also matters. Forcing a sleeve onto a contaminated or inadequately inflated mandrel can score the bore or leave the sleeve partially seated. A sleeve should be installed to its intended axial location without unusual resistance. Repeated difficulty fitting the same sleeve is evidence to inspect the sleeve bore and mandrel condition rather than merely increasing air pressure or force.
Thermal condition can complicate diagnosis. Sleeves, adapters, plates, and tapes do not necessarily respond identically to temperature. A component measured cold during maintenance may behave differently after the press reaches operating temperature. When symptoms occur only after warm-up, record the runout both before and after the relevant operating condition can be safely reproduced. This does not prove thermal expansion is the root cause, but it prevents a false “no fault found” conclusion based on a single cold inspection.
Use component substitution as a controlled test
When indicator readings show an issue but do not isolate the source, substitution can be more informative than repeated adjustment. Change only one element at a time and preserve the same measurement method. A known-good sleeve on the same mandrel tests the sleeve against the station. The suspect sleeve on another verified station tests whether the defect follows the sleeve. A known-good adapter can similarly separate adapter error from cylinder error.
Track the angular position of the high point after every change. If the defect follows the sleeve and maintains the same phase relative to a sleeve mark, the sleeve is implicated. If it remains at the same machine position regardless of sleeve orientation, the mandrel, bearing support, drive, or cylinder structure requires closer inspection. If the symptom disappears after cleaning and reinstallation, document the contamination or seating finding; otherwise the same fault is likely to return.
Substitution should not become a way to hide a developing mechanical problem. A cylinder bearing with early wear may show limited runout during a stationary hand rotation but develop movement under load and speed. If register drift is speed-sensitive, inspect bearing play, lubrication condition, drive coupling condition, and cylinder support according to the press maintenance procedure. Runout is one possible mechanism; structural movement under operating load is another.
When register control data is more useful than visual inspection
Modern register systems can provide evidence that is difficult to see on a printed sample. Repeating correction activity at a frequency linked to one print cylinder, especially when it grows with speed, supports a mechanical investigation. The key is correlation, not the absolute size of the correction. Compare the timing of register adjustments with cylinder rotational speed, defect repeat length, and indicator measurements.
A controller can compensate for slow or predictable errors within its correction range. It cannot remove the underlying variation in impression or restore a stable print nip if the sleeve radius changes during rotation. Excessive correction activity also masks the root cause: operators may keep chasing register while the press spends more time in correction than in stable production.
For this reason, avoid treating the register system as the first repair target when one unit shows a cyclic problem. Confirm the mechanical reference before recalibrating sensors, changing control gains, or modifying register parameters. Software changes can make the symptom less visible while leaving the sleeve, mandrel, or cylinder defect unresolved.
Build a usable runout record
A maintenance record should identify the press station, sleeve identification, adapter or mandrel identification, measurement locations, TIR readings, high-point positions, temperature condition, and whether the sleeve was reinstalled or moved to another station. It should also note the job symptom: color involved, direction of register movement, press speed at onset, and whether the behavior repeated once per revolution or at another frequency.
This level of documentation makes repeat faults easier to isolate. It also prevents an expensive sleeve from being rejected when the actual cause is a contaminated mandrel, worn bearing, or incorrect mounting build-up. Conversely, it prevents a damaged sleeve from being repeatedly returned to production because it happened to pass a visual inspection.
Sleeve runout in flexo is best treated as a traceable relationship between the printed defect and the rotating assembly. Measure from the machine reference outward, repeat the measurement after reinstallation, compare the phase of the high point, and test substitutions without changing several variables at once. That approach turns register drift from a vague production complaint into a mechanical fault that can be verified, contained, and repaired before it becomes a recurring source of waste and downtime.
Related News
 How an Impression Roller for Flexo Printing Affects Print QualityDiscover how an impression roller for flexo printing influences ink transfer, dot gain, alignment, and print consistency. Learn practical setup and troubleshooting tips.Print Fluidics Scientist
 Why Color Measurement Systems Matter for Consistent Flexo PrintingColor Measurement Systems help flexo printers achieve consistent brand colors, reduce waste, improve traceability, and protect packaging quality across every production run.Print Fluidics Scientist
 What to Check Before Choosing a Print Dryers Supplier for Your PressPrint dryers supplier selection guide: compare drying methods, press integration, energy use, maintenance, safety, and support to improve print quality and uptime.Print Fluidics Scientist
 How to Compare Web Tension Controller Manufacturers for Flexo PressesWeb tension controller manufacturer comparison guide for flexo presses: assess stability, sensing, integration, service, and real-world substrate performance.Print Fluidics Scientist
 How Hot Air Print Dryers Improve Ink Drying on Flexo LinesHot air print dryers improve flexo ink drying with balanced airflow, controlled heat, and reliable results for faster packaging production.Print Fluidics Scientist
 How to Choose a Plate Cylinder Manufacturer for Reliable Print QualityChoose a reliable plate cylinder manufacturer with proven precision, balance control, material expertise, and press compatibility for consistent print quality.Print Fluidics Scientist