For flexo press operators, stable ink viscosity is essential to achieving consistent color, clean solids, sharp graphics, and reliable production speeds.
Viscosity control systems for flexo press applications automatically monitor and adjust ink conditions, reducing shade variation, setup waste, and repeated manual correction during demanding production runs.
The practical value is straightforward: when ink viscosity remains within the correct operating window, the press delivers more predictable color transfer from startup through final sheet.
For operators, this means fewer density adjustments, less time chasing color changes, cleaner print appearance, and greater confidence when running repeat jobs or long corrugated orders.
Why Ink Viscosity Changes Become Visible Color Problems
Viscosity describes an ink's resistance to flow. In flexographic printing, it influences how ink circulates, fills anilox cells, transfers to the plate, and releases onto the substrate.
When viscosity rises, ink becomes thicker and flows less freely. This can reduce cell filling, alter transfer behavior, and create weak solids, dirty print, or uneven color density.
When viscosity drops too far, the ink may become overly fluid. Operators may see excessive color strength, dot gain, feathering, poor edge definition, or unstable printed solids.
Even small viscosity changes can affect print quality because flexo printing depends on a controlled relationship between ink, anilox volume, plate design, substrate, and press speed.
Water-based inks are especially sensitive to changing conditions. Evaporation can occur continuously in open chambers, ink trays, circulation tanks, hoses, and areas exposed to moving air.
As water evaporates, the remaining ink becomes more concentrated. Its viscosity rises, while pigment concentration, pH, drying behavior, and color strength can also shift.
Pressroom temperature and humidity also matter. A warm, dry plant can accelerate evaporation, while colder conditions can increase apparent viscosity and slow normal ink circulation.
Operators may first notice the issue as a density drift. The printed color can become lighter, darker, dirtier, or less uniform despite unchanged artwork, plates, anilox rollers, and settings.
On corrugated board, substrate variation can make diagnosis harder. Absorbency, liner quality, surface roughness, and moisture content may all influence how a viscosity change appears on board.
Without controlled viscosity, operators often respond by adjusting impression, doctor blade pressure, ink dilution, or anilox selection. Those corrections may hide the actual root cause.
How Viscosity Control Systems for Flexo Press Operations Work
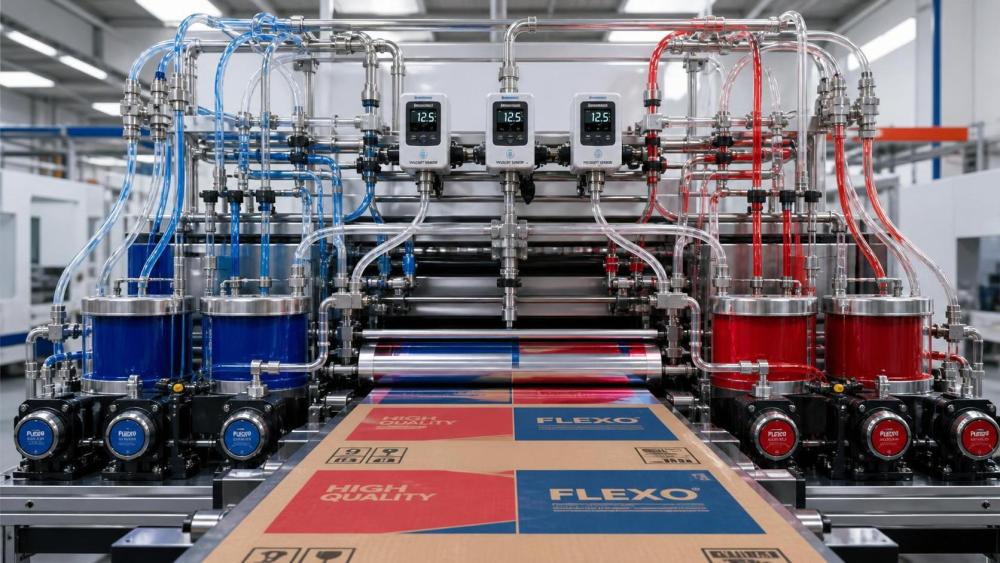
A viscosity control system measures ink condition in the circulation loop and adds controlled amounts of water, solvent, or approved reducer when the ink becomes too thick.
Most systems use a defined target value, often based on viscosity cup timing, electronic sensor readings, or a process-specific control parameter established during job setup.
The control unit compares the measured condition with the target. When viscosity exceeds the allowed range, it activates a dosing valve or pump for a calculated correction.
After dosing, the ink must circulate and mix before another reading is meaningful. Good systems account for this response time to prevent excessive dilution or unstable cycling.
In water-based flexo applications, the system usually adds water or a compatible dilution blend. In solvent-based printing, it may control the addition of selected solvent mixtures.
The system does not replace operator judgment. Instead, it keeps routine evaporation-related changes under control, allowing operators to focus on print appearance, registration, and process stability.
A basic setup may control one ink station at a time. More advanced installations can manage several colors independently while logging trends, alarms, additions, and operating history.
Some systems are integrated with ink supply units, pumps, return lines, and automatic washup equipment. Others are standalone units connected to existing circulation systems.
The important principle is closed-loop control. Ink condition is measured, corrected, mixed, checked again, and maintained close to the operating target throughout the production run.
For reliable results, the measurement point must represent actual press ink conditions. Poor tank placement, inconsistent circulation, air entrainment, or contaminated sensors can undermine control accuracy.
What Operators Should Expect During Startup and Long Runs
At startup, viscosity control helps the press reach stable conditions faster. It reduces the need for repeated manual cup checks while operators establish color, impression, and drying settings.
The first job target should not be copied blindly from a previous order. Ink batch, substrate, anilox condition, temperature, and artwork coverage can require a different operating point.
Once a visually acceptable print standard is approved, record the viscosity target together with anilox specification, press speed, pH, density readings, and substrate information.
That job record provides a practical starting point for repeat production. It also helps distinguish normal process variation from an incorrect setup or a developing equipment problem.
During long runs, the greatest benefit is consistency over time. A controlled ink loop prevents gradual thickening from becoming a visible color shift several thousand sheets later.
Operators should still inspect print regularly. Automated viscosity control stabilizes one critical input, but it cannot correct worn plates, plugged anilox cells, poor doctor blades, or substrate defects.
Color checks should combine visual comparison with measurable methods where available. Density, spectral data, barcode verification, and approved drawdown samples support more reliable decisions.
When a color change appears despite stable viscosity, investigate other variables systematically. Check ink temperature, pH, anilox cleanliness, circulation flow, plate condition, impression, and board consistency.
This disciplined approach prevents unnecessary dilution. Adding water to solve every print problem can weaken color strength, change drying performance, and create new quality issues downstream.
For unattended or lightly staffed shifts, alarms are particularly useful. Alerts for high viscosity, low supply level, pump failure, sensor faults, or excessive dosing protect production stability.
Setting the Right Viscosity Target for Each Job
There is no universal viscosity number for every flexographic job. The correct target depends on ink chemistry, printing method, substrate, anilox volume, image coverage, and required color result.
Begin with the ink supplier's recommended operating range. Then confirm the best production target through approved press trials using the actual substrate and normal running speed.
High-coverage solids may require different behavior than fine text, linework, or process screens. A target that produces strong solids can be unsuitable for delicate highlight dots.
Corrugated post-printing creates additional variables. Board flute profile, liner absorbency, warp, surface contamination, and compression characteristics can affect the visible result at the same ink setting.
Operators should avoid selecting a target only by cup seconds without context. Different cups, temperatures, measurement methods, and ink formulations can produce misleading comparisons.
Use one consistent method within the plant. Document which cup, temperature range, measurement location, and timing procedure apply to each job and each ink family.
Electronic systems should also be validated against the plant's accepted reference method. A sensor reading is useful only when operators understand how it relates to production quality.
Set an acceptable control band rather than expecting an unrealistically fixed number. The goal is stable color within specification, not constant adjustment in response to insignificant variation.
A narrow band may be appropriate for demanding brand colors or high-graphics work. A broader band may be practical for less sensitive transport packaging applications.
Document changes made during the run. If the operator adjusts the target, the reason should be clear: ink batch variation, substrate change, approved color correction, or process investigation.
Common Problems That Limit System Performance
Automatic control cannot compensate for poor ink circulation. If the tank does not mix evenly, the sensor may read one condition while the print unit receives another.
Air bubbles are a frequent source of unstable readings and poor transfer. Check suction lines, pump seals, return flow, low ink levels, and excessive agitation.
Sensor contamination can also create false control actions. Dried ink, foam, pigment buildup, or cleaning residue may cause the system to add unnecessary water or solvent.
Follow a regular cleaning schedule based on ink type and production volume. Include the sensor, sample chamber, valves, filters, hoses, and any measurement cup components.
Incorrect dosing calibration is another risk. If a pump adds more reducer than expected, the system can overshoot the target and create a repeated cycle of correction.
Verify pump output at planned intervals. Measure actual delivery volume, inspect tubing condition, and replace worn components before they affect print stability or process records.
In water-based systems, pH should not be ignored. Viscosity may appear controlled while pH drifts outside the ink supplier's recommended range, affecting color and drying behavior.
Likewise, ink temperature should be monitored where production conditions change substantially. Temperature can alter viscosity readings and printing response even when the formulation remains unchanged.
Operators should be cautious when switching ink batches. New ink may require different starting conditions, especially when pigment strength, resin content, or supplied viscosity differs from prior stock.
A proper handover procedure reduces surprises. Record current targets, additions, quality observations, alarms, pending maintenance, and any known issues before the next shift takes control.
Daily Operator Checks That Protect Color Consistency
Before production, confirm that the ink supply is correctly identified and compatible with the job. Check the tank level, circulation direction, filters, hoses, valves, and return flow.
Inspect the sensor or measurement device for cleanliness. Verify that it is properly installed, connected, and able to receive representative ink without trapped air or dry residue.
Confirm the target setting against the approved job record. Do not rely on a previous shift's display value without checking the order, ink color, substrate, and press unit.
During make-ready, compare automated readings with the plant's reference procedure. A quick manual verification can identify calibration issues before they cause avoidable setup waste.
Watch the trend, not only the current number. A system that requires unusually frequent additions may indicate excessive evaporation, a leak, incorrect target settings, or sensor trouble.
Observe dosing frequency after major changes in speed, temperature, or coverage. Press conditions can change rapidly when moving from low-coverage graphics to heavy solid-color production.
At washup, clean the system according to the ink supplier and equipment manufacturer's recommendations. Incomplete cleaning increases contamination risk when the next color or ink system is loaded.
After washup, check that drains, filters, and measurement lines are clear. Residual material can compromise the next run, especially with light colors or tightly specified brand shades.
Choosing a System That Fits the Pressroom
When evaluating viscosity control systems for flexo press use, begin with the press configuration. Consider ink type, number of stations, circulation layout, tank size, and expected production volume.
Ask whether the system supports the specific ink chemistry used in the plant. Water-based, solvent-based, UV, and specialty inks may require different control methods and materials.
Assess measurement reliability under real operating conditions. The system should handle normal pigment levels, temperature variation, foam risk, cleaning routines, and production speeds without frequent intervention.
Review the dosing method carefully. Accurate, repeatable dosing pumps and compatible valves are more valuable than a complicated interface that operators cannot maintain or troubleshoot.
For multi-color presses, independent control by station is usually important. Different colors can evaporate, circulate, and print differently, particularly when coverage varies between units.
Data logging can be useful for quality investigation and repeatability. Trend records help supervisors identify recurring instability, compare shifts, and improve standard operating procedures.
However, data should support action. Choose reporting features that the production team will actually review, rather than paying for complex functions that remain unused after installation.
Serviceability matters in busy packaging plants. Operators need accessible filters, clear alarms, available spare parts, understandable calibration steps, and technical support familiar with flexo processes.
Installation should include commissioning with production inks and representative jobs. Acceptance testing should confirm stable control, correct dosing, safe operation, and measurable print-quality improvement.
Building a More Repeatable Flexo Color Process
Viscosity control is most effective when it is part of a broader color-management routine. Stable ink condition must work alongside clean anilox rollers, controlled plates, and consistent substrates.
Maintain anilox rollers using documented cleaning practices. Reduced cell volume changes ink delivery and can look like a viscosity problem, leading operators toward incorrect adjustments.
Keep doctor blade settings consistent and replace worn blades promptly. Streaks, haze, scoring, and poor wipe quality can affect solids and make color instability harder to diagnose.
Standardize the process for ink preparation. Record initial viscosity, pH where relevant, temperature, batch information, and approved additives before ink reaches the press circulation system.
Create a simple escalation path for operators. Define when they should correct a setting, when they should call maintenance, and when quality personnel should review a color deviation.
Train operators to use the control system as process information, not merely an automatic water-addition device. Trends often reveal issues before they become costly visible defects.
Consistent color is not achieved by automation alone. It comes from controlling the variables that matter most, recording successful settings, and responding to changes with evidence.
Conclusion: Control the Ink Condition Before Chasing the Color
For flexo press operators, viscosity control systems provide a practical way to reduce one of the most common causes of color drift: changing ink condition during production.
They help maintain cleaner solids, more predictable shade, improved repeatability, and fewer manual corrections when configured correctly and supported by disciplined daily checks.
The best results come from matching the system to the ink and press, setting job-specific targets, maintaining the circulation loop, and verifying print quality throughout the run.
When viscosity is stable, operators can diagnose other color variables more accurately. That improves production control, reduces waste, and supports reliable packaging print quality across every shift.