How Sheet Stackers for Flexo Press Reduce Manual Handling Delays
A sheet stacker reduces manual handling delays only when it receives, aligns, lowers, and releases printed sheets at the same pace as the flexo press. If the stacker repeatedly stops the press, produces leaning piles, damages fresh print, or forces operators to square every load by hand, it has become a bottleneck rather than an automation point.
For maintenance work, the useful question is not simply whether the stacker runs. It is whether the delivery section can accept normal variation in sheet size, board stiffness, print condition, and production speed without creating intervention cycles. Reliable sheet stackers for flexo press lines keep the operator out of the repeated lift-and-correct routine, protect sheet orientation for the next process, and allow the press to maintain a stable delivery rhythm.
Where manual handling delays begin
Manual handling usually appears after a small instability has already developed. A sheet may enter the stacker slightly skewed, arrive with too much speed, curl at one edge, or fail to settle before the next sheet lands. Operators then compensate by straightening piles, removing damaged sheets, separating doubled sheets, or clearing a delivery jam. Each intervention may be brief, but the accumulated effect is slower output, inconsistent stack quality, and more frequent press slowdowns.
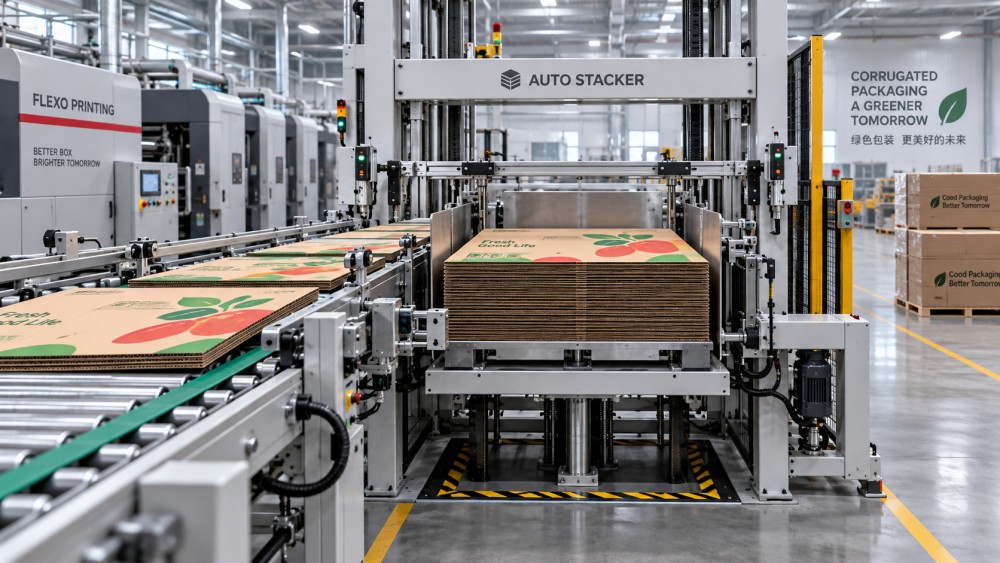
The stacker has to perform several actions in sequence: receive the sheet, control its deceleration, register it against side and front references, support the growing pile, lower the pile at the correct rate, and discharge it without disturbing the top sheets. A fault at any point can be interpreted as an operator problem when it is actually a machine-setting, mechanical, pneumatic, electrical, or material-handling issue.
Maintenance teams should therefore treat the stacker as part of the press delivery system, not as a separate accessory at the end of the line. Its performance depends on the condition and timing of upstream belts, transfer rollers, vacuum devices where fitted, delivery gates, sheet guides, and the interface to downstream conveying or pallet handling.
How a stable stacker removes the handling work
At a basic level, automation reduces handling by replacing repeated human corrections with controlled sheet positioning. The practical value comes from consistency rather than from a single high-speed movement.
When a sheet enters squarely and is stopped in a controlled manner, the pile remains usable for bundling, die-cutting, folder gluing, inspection, or transfer to another process. Operators do not need to pause the line to rebuild the stack. When the lift table lowers smoothly as pile height increases, the drop distance remains controlled, so printed surfaces are less likely to scuff and lightweight sheets are less likely to shift. When completed piles are released predictably, forklifts, pallet jacks, or downstream conveyors can collect them without waiting for manual re-squaring.
This is especially relevant for corrugated sheets and printed board because material behavior can change from job to job. A stacker adjusted for flat, rigid sheets may not handle lighter board, warped material, high-coverage ink areas, or sheets with a tendency to curl in the same way. The right response is not to add more manual labor at delivery. It is to identify which part of sheet control has lost its operating margin.
Start fault finding with the pile, not the alarm screen
Alarms matter, but the finished stack often identifies the fault more quickly than a message on the HMI. The direction of skew, the location of scuffing, the height at which instability begins, and whether the problem occurs at a particular press speed all point toward different causes.
A pile that drifts in one direction from the first sheets usually indicates an entry or guide alignment problem. A pile that remains stable and then becomes loose at a certain height often points to lift-table descent, pile-height sensing, or excessive sheet drop. Damage concentrated on a leading edge may indicate an aggressive front stop or mistimed deceleration. These distinctions prevent maintenance work from becoming a cycle of random parameter changes.
The adjustments that have the greatest effect
Sheet entry and belt condition. A stacker cannot correct a sheet that enters with unstable tracking. Check belt wear, contamination, tracking, tension consistency, roller condition, and any transfer elements that influence sheet angle before it reaches the stacking zone. Worn belts or uneven roller surfaces can produce minor tracking variation that becomes a visibly crooked pile after many sheets.
Side-guide position and parallelism. Guides should support repeatable registration without pinching the sheet. Too much clearance allows side drift; too little clearance can mark edges, slow the sheet, or create a buckle as material passes through. Parallelism matters as much as the displayed guide width. One guide set slightly out of square can create a persistent lean that operators later have to correct by hand.
Front-stop action and deceleration. The goal is controlled settling, not the fastest possible stop. If deceleration is too abrupt, sheets can rebound, fan, or mark. If it is too weak, sheets may overrun the registration point. Review the timing together with actual production conditions. A setting that works at low speed may become unstable when the press accelerates, and a setting suited to rigid board may be unsuitable for lighter material.
Lift-table descent and pile-height control. A stable stack needs a reasonably consistent landing distance. If the table descends too late, sheets fall too far and lose alignment. If it descends too early or inconsistently, the delivery area may not support proper settling. Inspect lift chains, screws, guides, bearings, drive components, and lubrication according to the equipment design. Sensor cleanliness, bracket rigidity, reflector position, and cable movement also deserve attention because intermittent height feedback can look like a mechanical problem.
Air and vacuum systems. Pneumatic stops, blowers, sheet separation devices, and vacuum-supported transport depend on clean, dry air and stable pressure. Leaks, blocked filters, degraded valves, and contaminated solenoids often produce intermittent faults rather than a complete failure. That makes them easy to overlook during a quick inspection. A repeatable test at operating speed is more useful than confirming that a cylinder moves during idle mode.
Do not tune the stacker in isolation
A frequent mistake is to adjust the stacker only after sheets have already arrived poorly controlled. Delivery quality begins upstream. Sheet curl can be affected by board condition, moisture balance, converting stress, print coverage, drying or curing conditions, and transport settings. Registration variation from the press or die-cutting section can also reach the stacker as an apparent delivery fault.
This does not mean every stack problem originates upstream. It means the maintenance sequence should follow the material path. Confirm that sheets leave the preceding section consistently, then verify transfer stability, then inspect the stacker’s alignment and lift functions. Changing side-guide settings before checking entry tracking may hide the symptom for one job and worsen it for another.
Short-run work deserves particular attention. Frequent changes in sheet dimensions, flute profiles, print coverage, and pile requirements reduce the value of a stacker if its setup is entirely dependent on operator memory. Where the controls support recipes, maintain a practical record of approved guide positions, delivery timing, lift behavior, and material-specific notes. The record should describe the operating condition, not merely store a job name. This makes fault recovery faster and helps distinguish a bad setting from a developing mechanical issue.
Build preventive maintenance around delay patterns
Scheduled maintenance is more effective when it addresses the conditions that cause operators to intervene. A checklist limited to “machine running” can miss the gradual changes that lead to stack quality problems.
- Inspect and clean photoelectric sensors, reflectors, encoder targets, and moving cables that affect sheet or pile-height detection.
- Check guides, stops, linkages, fasteners, and brackets for looseness, wear, or movement under operating vibration.
- Verify belt tracking and roller cleanliness, especially where ink dust, paper debris, adhesive residue, or coating buildup can alter grip.
- Examine lift mechanisms for abnormal noise, backlash, uneven movement, lubrication failure, and signs that the table is not remaining level.
- Test pneumatic devices under normal production conditions, including repeated cycling at realistic speed.
- Review recurring operator interventions by job type, material, shift, and stack position rather than treating each event as unrelated.
The last point is often the most useful. A repeated need to correct stacks at the same pile height suggests height control or lift motion. A problem limited to one board grade suggests a setting range or material-handling limitation. A fault that appears after wash-up or cleaning may point to contamination, displaced sensors, or a connection disturbed during service. Patterns turn maintenance records into diagnostic information.
When a stacker upgrade is justified
Not every manual-handling delay requires replacement. Alignment correction, worn components, sensor service, improved recipes, and better coordination with upstream delivery can restore stable operation. An upgrade becomes more relevant when the existing stacker cannot support the actual production mix: changing sheet sizes require excessive manual setup, the pile cannot be discharged in a way that matches downstream logistics, controls do not provide usable fault information, or the system lacks the capacity to maintain sheet control at the press’s normal working speed.
For a replacement or retrofit evaluation, compare the full material path. Confirm maximum and minimum sheet formats, board thickness and stiffness range, print-surface sensitivity, required pile height, discharge method, available floor layout, interface signals, guarding, and downstream equipment. A stacker that looks suitable on a specification sheet can still create delays if it does not match the press delivery geometry or the way finished loads are moved through the plant.
Global Commercial Print & Corrugated Packaging Intelligence (CPCS) approaches flexographic and packaging automation as connected production systems. In this context, delivery equipment should be assessed alongside press output, converting flow, inspection needs, and end-of-line handling. The useful investment question is not whether the stacker is automated, but whether it removes a recurring source of waiting, rework, and operator intervention across the whole workflow.
FAQ
Can better stacker settings compensate for warped corrugated sheets?
They can reduce the impact, but they cannot fully correct severe or inconsistent warp. Check the condition of sheets entering the delivery section first. Guide position, deceleration, and lift-table control should then be adjusted to avoid adding instability.
Why does a stack stay square at low speed but fail at production speed?
The sheet has more momentum, and timing margins become smaller. Review entry tracking, deceleration, front-stop timing, guide pressure, and lift descent while the press runs at the speed where the issue occurs.
Should side guides be set tightly to keep sheets square?
No. Tight guides can drag edges, cause buckling, and mark printed surfaces. The correct setting controls lateral movement while allowing the sheet to travel freely into the stack.
What should be checked first after a stacker starts stopping intermittently?
Begin with sensor condition, cable movement, pile-height feedback, and mechanical freedom of the lift table. Intermittent stops often come from unstable detection or a movement issue that only appears during repeated cycles.
Related News
 How Quick Change Unwind Stands Reduce Downtime on Flexo PressesDiscover how quick change unwind stands reduce flexo press downtime, streamline reel changes, and improve productivity—plus key tips to assess integration and ROI.Print Fluidics Scientist
 How an Impression Roller for Flexo Printing Affects Print QualityDiscover how an impression roller for flexo printing influences ink transfer, dot gain, alignment, and print consistency. Learn practical setup and troubleshooting tips.Print Fluidics Scientist
 Why Color Measurement Systems Matter for Consistent Flexo PrintingColor Measurement Systems help flexo printers achieve consistent brand colors, reduce waste, improve traceability, and protect packaging quality across every production run.Print Fluidics Scientist
 What to Check Before Choosing a Print Dryers Supplier for Your PressPrint dryers supplier selection guide: compare drying methods, press integration, energy use, maintenance, safety, and support to improve print quality and uptime.Print Fluidics Scientist
 How to Compare Web Tension Controller Manufacturers for Flexo PressesWeb tension controller manufacturer comparison guide for flexo presses: assess stability, sensing, integration, service, and real-world substrate performance.Print Fluidics Scientist
 How Hot Air Print Dryers Improve Ink Drying on Flexo LinesHot air print dryers improve flexo ink drying with balanced airflow, controlled heat, and reliable results for faster packaging production.Print Fluidics Scientist