Dimensional Stability in Flexo Sleeves: What to Test Before Approval
A flexo sleeve can appear acceptable during a brief press trial and still create costly registration, impression, or repeatability problems once production conditions change. For technical approval, dimensional stability should be treated as a system-performance requirement: the sleeve must retain its intended geometry during mounting, rotation, compression, cleaning, storage, and exposure to the press environment.
The practical question is not whether a sleeve meets one nominal diameter when it leaves the supplier. It is whether its diameter, wall structure, concentricity, and surface behavior remain predictable on the specific press, bridge, adapter, plate-mounting method, and job mix for which it is being approved. A sleeve that changes dimension only slightly can still affect print repeat, color-to-color register, dot reproduction, and setup time, particularly on long runs or jobs with tight graphic tolerances.
Technical evaluators should therefore approve dimensional stability flexo sleeves through a controlled sequence of incoming measurement, mounting checks, running evaluation, and post-use inspection. The objective is to identify instability before the sleeve becomes part of normal production.
Start With the Press Requirement, Not the Sleeve Specification
Nominal repeat length is the first reference point, but it is not enough for approval. A sleeve is part of a rotating assembly that includes the air mandrel or cylinder, bridges or adapters where used, mounting tape, plate material, and the printing plate itself. Each component contributes to the effective print circumference and to the way that circumference behaves under load.
Before comparing suppliers or material constructions, define the operating condition that the sleeve must support. A sleeve used for solid corrugated post-printing at moderate graphic demands does not face the same approval criteria as a sleeve used for fine screens, process work, or narrow registration tolerances. Likewise, a sleeve that stays on one press and one repeat may be easier to control than a sleeve expected to move between presses, adapters, or production sites.
The approval brief should identify the items that create dimensional risk in the intended application:
- Required print repeat and permitted registration variation.
- Press type, mandrel diameter, air-hole pattern, and mounting procedure.
- Maximum production speed, expected run length, and normal acceleration or deceleration profile.
- Plate type, plate thickness, tape construction, and mounting-tape compression.
- Ink, wash-up chemistry, cleaning method, and drying temperature around the print unit.
- Expected storage conditions and the frequency of sleeve handling or changeovers.
This step prevents a common approval error: accepting a sleeve based on dimensional figures that were measured in a condition unrelated to the production assembly. A supplier may correctly state a nominal inside diameter, wall thickness, or repeat capability, while the mounted sleeve still produces an unstable effective circumference because the press interface or compressible layers behave differently under operating load.
Measure Geometry in More Than One Direction
Diameter consistency deserves close attention because it influences print repeat directly. However, a single diameter reading at one location cannot establish that a sleeve is geometrically stable. The evaluation should examine dimensions along the sleeve length and around its circumference. This reveals whether the sleeve is round, cylindrical, and uniform rather than merely close to nominal at one measurement point.
Useful incoming checks include inside diameter, outside diameter where relevant to the sleeve construction, wall thickness, length, and concentricity. Measurements should be repeated at multiple axial locations and angular positions. The purpose is to find local variation, taper, ovality, or thickness changes that can become visible as inconsistent impression or register behavior at press speed.
Wall thickness deserves separate treatment. In a base sleeve, variation in wall thickness can change stiffness and alter the relationship between the inner bore and printing surface. In a compressible or coated sleeve, thickness variation may also produce uneven compression across the print width. A sleeve can mount securely and still show localized pressure differences when the plate, tape, and print surface rotate through the nip.
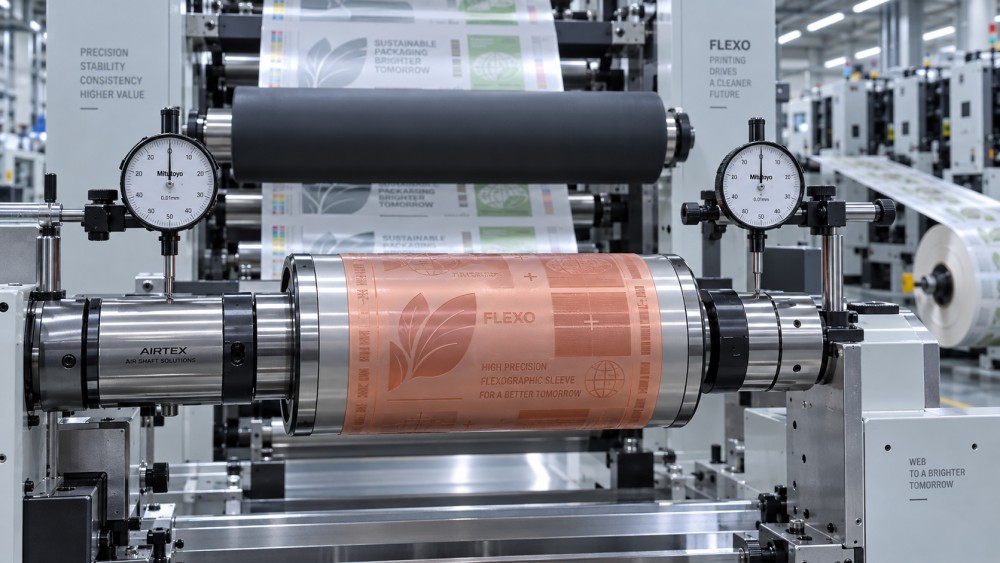
Runout is equally important. Radial runout describes variation in the printing surface as the sleeve rotates. Excessive runout can produce cyclical changes in impression, ink transfer, and dot gain. Axial runout or face wobble can complicate lateral register, especially on jobs where graphics, barcodes, or fine lines approach the edge of the image area. These effects may be more obvious after the sleeve is mounted than during bench inspection, so both stages matter.
Measurements should be documented with the same reference method for every sleeve sample. Comparing readings taken with different fixtures, gauges, temperatures, or support conditions can create false disagreement between supplier data and plant inspection data. The measurement process must distinguish a true sleeve deviation from variation introduced by handling or test equipment.
Mounting Fit Is a Dimensional Test
A sleeve’s fit on the mandrel is often described as a handling issue, but it is also a dimensional stability test. The sleeve should expand adequately under the available air supply, slide onto the mandrel without damaging its bore, seat fully in the intended position, and contract into a stable running fit after air is removed. Difficult mounting can indicate a bore mismatch, internal surface issue, inadequate air distribution, or a sleeve construction that is overly sensitive to temperature or handling.
Approval should include repeated mount-and-dismount cycles, not only the first installation. A sleeve that performs well when new may behave differently after cleaning, storage, plate removal, or repeated expansion. The inspection should look for changes in bore condition, cracking, softening, delamination, edge damage, or loss of mounting consistency. These conditions can affect sleeve geometry before an obvious failure occurs.
The interface between sleeve and mandrel must also be clean and controlled during evaluation. Dust, tape fragments, dried ink, moisture, or damage on the mandrel can raise the sleeve locally and imitate a runout problem. If the test setup is not clean, the team may reject a sound sleeve or approve one whose variability is hidden by inconsistent mounting practice.
For sleeves used with bridges or adapters, the approval assembly should match the production assembly. Each additional interface creates another tolerance stack. A stable sleeve on a direct mandrel can behave differently when mounted over an adapter with its own runout, wear pattern, or thermal response. Measuring only the sleeve outside the complete rotating system leaves an important source of error untested.
Assess Compression as a Dynamic Behavior
Dimensional stability is sometimes reduced to hard geometry, yet the print surface is exposed to compression at every impression point. The relevant issue is not simply whether the sleeve is hard or soft. It is whether the sleeve, tape, and plate package compresses consistently, recovers predictably, and remains stable across the width and through the run.
A compressible construction can be useful where it supports controlled ink transfer or accommodates certain substrate conditions. It can also introduce more variables into repeatability if compression varies by location, changes with load, or fails to recover after a stop. Technical approval should therefore evaluate the sleeve under representative impression settings rather than relying only on static hardness descriptions.
During a press trial, examine whether adjustment of impression produces a uniform response across the web or sheet width. Watch for repeated density changes, uneven solids, localized dot gain, or a print defect that repeats at the sleeve circumference. Those symptoms do not prove that the sleeve is the cause, but they justify checking sleeve runout, wall uniformity, mounting condition, plate mounting, and tape compression as one system.
Recovery after compression is particularly relevant for jobs with stops, frequent speed changes, or repeated order changes. A sleeve that requires a long period to return to stable dimensions after an interruption can add waste during restart. The risk is not limited to visible print defects. Operators may compensate with impression or register adjustments that make the job harder to return to a known condition.
Test Thermal and Chemical Exposure at the Right Level
Temperature changes can alter sleeve dimensions directly or influence the stiffness of polymers, adhesive layers, tapes, and mounted plates. The effect may be small in a controlled room and more visible after the press has run, after local heat has built up around drying equipment, or when sleeves move between storage and production areas with different temperatures.
Approval should include a comparison between measurements taken before use and after a representative running period. Where the process includes elevated temperatures, the team should observe whether register drifts as the press reaches normal operating conditions and whether dimensions return consistently after cooling. The aim is to identify repeatable behavior, not to assume that every dimensional change is unacceptable. A predictable response can often be managed; an erratic one is much harder to control.
Wash-up and cleaning procedures deserve the same attention. Solvent exposure, aggressive cleaning agents, prolonged soaking, or mechanical scrubbing can affect surface coatings, adhesives, foam layers, and internal structures depending on sleeve design. A sleeve may retain its nominal diameter while losing surface integrity or local stiffness. That can later show up as uneven print pressure or shortened usable life.
The approval process should use the plant’s intended ink and cleaning regime where possible. Generic chemical-resistance statements are useful only as a starting point. The operational question is whether the sleeve remains dimensionally and mechanically consistent after the specific exposure sequence that operators will repeat over its service life.
Separate Sleeve Problems From Plate and Tape Problems
Registration drift is often attributed to the sleeve because the sleeve establishes the print circumference. In practice, the defect may originate in plate stretch, inconsistent mounting tape, uneven tape seams, adhesive creep, incorrect plate mounting, or changes in web tension. Approval becomes more reliable when evaluators isolate these variables.
A practical method is to establish a controlled baseline using known, stable plates and tape. Test the sleeve with the same mounting procedure, operator instructions, press settings, and inspection method used for the comparison sleeve. If the new sleeve produces different results, the team has a stronger basis for further investigation. If all variable components change between trials, the test may demonstrate only that two different assemblies print differently.
Plate mounting should be inspected for air entrapment, tape overlap, inconsistent tape thickness, plate-edge lift, and circumferential alignment. These details can create localized effects that resemble sleeve distortion. The sleeve should not be approved simply because the trial was acceptable after extensive operator correction. Approval has more value when the assembly reaches stable print quality through a repeatable normal setup.
Use Production-Relevant Acceptance Criteria
There is no universal single tolerance that can approve every flexo sleeve. The acceptable range depends on print repeat, artwork sensitivity, substrate behavior, press condition, and the degree to which downstream quality requirements tolerate register movement. A broad corrugated graphic, for example, may remain acceptable under variation that would be unacceptable for fine process graphics, small type, security elements, or machine-readable codes.
For that reason, an approval record should link dimensional findings to observed press performance. It should record the sleeve identity, repeat, material or construction, measurement method, mandrel or adapter used, plate-and-tape package, operating conditions, print observations, and post-trial inspection results. This creates a usable reference for future purchases, troubleshooting, and repeat-order qualification.
The record should also distinguish between initial conformance and durability. A new sleeve can meet geometric requirements on day one while showing deterioration after repeated mounting or cleaning. When the intended duty cycle is demanding, approval should include an early-life follow-up inspection after controlled use rather than treating the first press run as the final evidence.
Approval Should End With a Repeatability Decision
The strongest approval outcome is not simply “prints well.” It is evidence that the sleeve mounts consistently, rotates within the required geometric control, maintains stable behavior under representative compression and temperature conditions, and returns to the same usable state after normal handling. That is what protects setup efficiency and registration performance across more than one run.
For technical evaluators, the most useful question at each stage is simple: can this sleeve be returned to a known press condition without exceptional adjustment? If the answer depends on unusual handling, narrow environmental conditions, or repeated operator intervention, the sleeve may be technically usable but not yet robust enough for routine approval.
Related News
 How Quick Change Unwind Stands Reduce Downtime on Flexo PressesDiscover how quick change unwind stands reduce flexo press downtime, streamline reel changes, and improve productivity—plus key tips to assess integration and ROI.Print Fluidics Scientist
 How an Impression Roller for Flexo Printing Affects Print QualityDiscover how an impression roller for flexo printing influences ink transfer, dot gain, alignment, and print consistency. Learn practical setup and troubleshooting tips.Print Fluidics Scientist
 Why Color Measurement Systems Matter for Consistent Flexo PrintingColor Measurement Systems help flexo printers achieve consistent brand colors, reduce waste, improve traceability, and protect packaging quality across every production run.Print Fluidics Scientist
 What to Check Before Choosing a Print Dryers Supplier for Your PressPrint dryers supplier selection guide: compare drying methods, press integration, energy use, maintenance, safety, and support to improve print quality and uptime.Print Fluidics Scientist
 How to Compare Web Tension Controller Manufacturers for Flexo PressesWeb tension controller manufacturer comparison guide for flexo presses: assess stability, sensing, integration, service, and real-world substrate performance.Print Fluidics Scientist
 How Hot Air Print Dryers Improve Ink Drying on Flexo LinesHot air print dryers improve flexo ink drying with balanced airflow, controlled heat, and reliable results for faster packaging production.Print Fluidics Scientist