What Shapes Intermittent Motion Drive Price in Modern Carton Lines
For procurement teams in modern carton plants, intermittent motion drive price is rarely determined by one single component. In most cases, the quoted price reflects a combination of motion accuracy, duty cycle strength, control integration, changeover requirements, maintenance design, and supplier support. Buyers who evaluate only the initial equipment price often miss the factors that shape long-term running cost and production stability.
That is the core search intent behind this topic. Procurement managers are usually not asking for a simple market number. They want to understand why one intermittent motion drive system costs more than another, which technical differences are commercially meaningful, and how to judge whether a higher price is justified in a carton converting environment.
For this audience, the most important questions are practical. They want to know what actually drives price, which specifications matter in real production, where hidden cost appears after installation, and how to compare suppliers without being misled by incomplete quotations. The most useful content therefore is not broad theory, but a structured buying framework linked to uptime, speed, maintenance, and lifecycle value.
In this article, the focus stays on those decision points. It highlights the price-forming variables that matter in modern carton lines, explains where premium pricing can create real operational return, and shows where buyers should be cautious about paying extra for features that do not match plant needs.
Why intermittent motion drive price varies so much in carton converting equipment
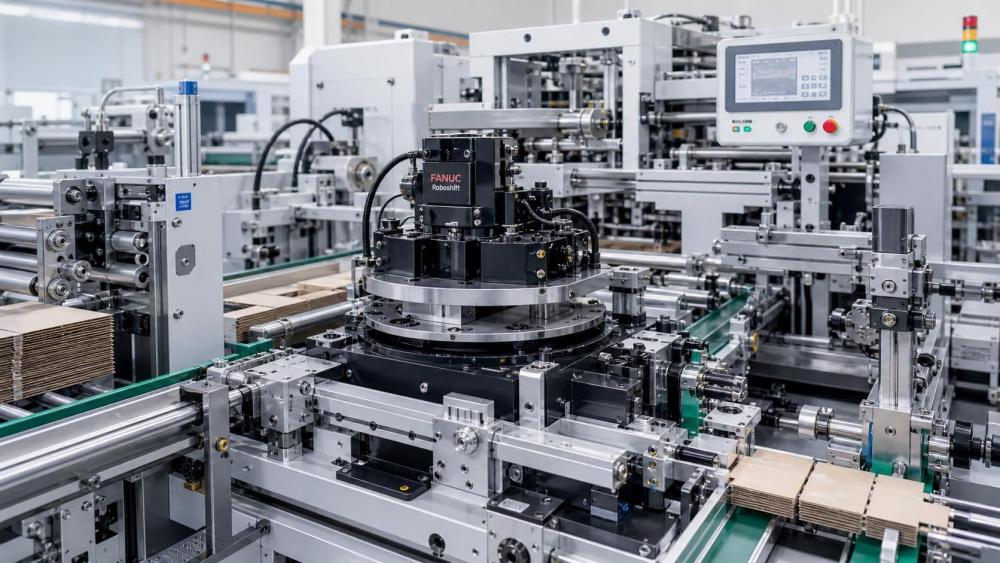
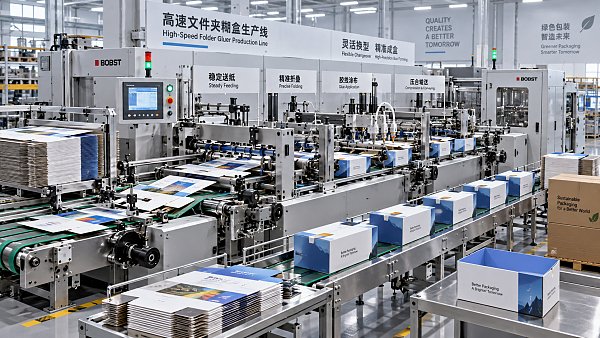
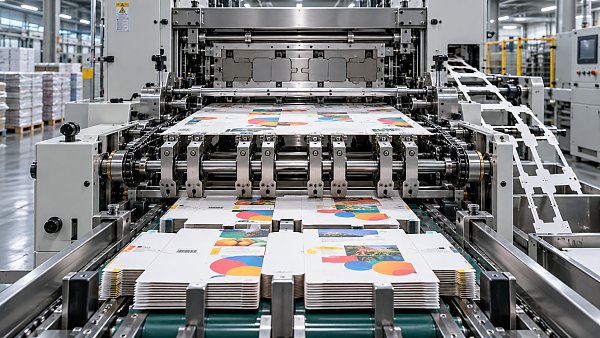
In carton production, intermittent motion systems are used where materials must stop, index, position, fold, glue, cut, stamp, or register with high repeatability. This is common in folder gluers, die-cutting support modules, feeding sections, coding units, inspection stations, and specialized transfer mechanisms.
Because these applications differ in speed, load, accuracy, and line integration, intermittent motion drive price can vary widely. A drive designed for moderate indexing in a simple feeder will not be priced like a high-cycle servo-driven indexing unit that must hold registration under continuous production pressure.
For procurement teams, the first principle is simple. Price rises when the drive must deliver tighter positioning accuracy, higher cycle frequency, stronger torque stability, longer service life, and easier synchronization with the broader machine control system. The quotation is usually a reflection of performance risk transferred from the buyer to the supplier.
That means a cheaper drive is not automatically the better buy. If lower cost comes with weaker repeatability, faster wear, or more downtime, the total operating result may be worse even when the purchase price looks attractive during tender comparison.
Which technical factors have the biggest impact on price
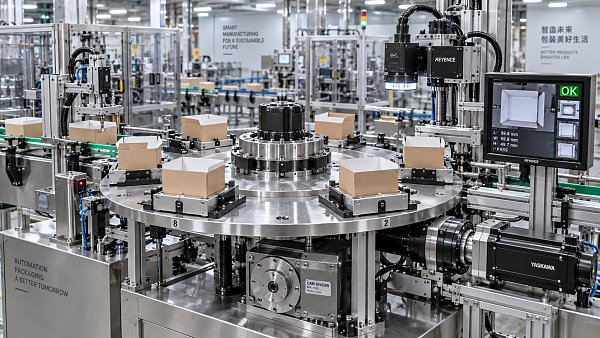
The largest pricing differences usually come from drive architecture. Mechanical cam-based intermittent drives, servo indexing systems, and hybrid motion platforms each have different cost structures. Traditional mechanical systems can be cost-effective in stable, repetitive production, while servo-based solutions often cost more because they offer flexible motion profiles and faster changeover capability.
Torque capacity is another major factor. A drive handling heavier board grades, larger carton blanks, or aggressive acceleration profiles needs stronger internal construction, better bearings, more robust housings, and higher-grade power transmission elements. Those upgrades directly affect intermittent motion drive price.
Positioning accuracy also matters. In modern carton lines, especially where printing registration, gluing placement, coding position, or die-cut alignment must remain stable, higher accuracy drives command higher prices. This is because precision depends on tighter machining tolerances, better feedback systems, and more advanced control logic.
Speed rating has a similar effect. Many buyers look only at nominal machine speed, but intermittent motion units are priced according to how consistently they can perform at high cycling rates without overheating, vibration, backlash growth, or unstable indexing. Reliable high-speed operation is expensive because it requires stronger engineering margins.
Control compatibility can also raise cost. Drives that integrate smoothly with PLC platforms, HMI recipes, encoder feedback, and line-level automation usually cost more upfront, but they reduce engineering complexity during installation and help support future upgrades in connected production environments.
How durability and maintenance design influence real purchasing value
Procurement decisions in carton plants should not treat drive price as separate from maintenance behavior. In many factories, the real financial difference between two intermittent drive options appears only after months of continuous production, when lubrication intervals, spare part wear, and unplanned stops begin to affect output.
A lower-cost drive may use more basic bearings, seals, cam profiles, or gearbox materials. That may be acceptable in low-duty applications, but in high-output converting lines it often results in more frequent adjustments, part replacement, and service intervention. These costs are rarely visible in the first quotation.
By contrast, a higher intermittent motion drive price may reflect sealed lubrication systems, stronger wear surfaces, modular replacement design, and easier maintenance access. These features matter because carton plants increasingly run shorter lead times and tighter delivery schedules. Maintenance-related stops are now commercially more damaging than many buyers assume.
Durability is especially important where the drive operates in dusty environments, around paper fibers, glue exposure, vibration, or repeated shock loading. If the supplier cannot explain how the drive is protected against these conditions, the low price may be masking lifecycle risk.
For procurement teams, one of the best questions is not only how long the unit lasts, but how failure happens. Predictable wear with planned service is manageable. Sudden failure that stops a converting line during customer orders is much more expensive than the price gap between two drive options.
Why control flexibility and changeover speed are now part of the price discussion
Modern carton plants are no longer optimized only for long, uniform production runs. Many operations now face mixed order sizes, frequent SKU changes, tighter branding requirements, and more traceability tasks. In this environment, intermittent motion systems are increasingly evaluated by how fast they support setup and changeover.
Servo-driven intermittent systems generally carry a higher price because they can store recipes, adjust motion electronically, and reduce manual intervention between jobs. For plants producing varied carton formats, this flexibility can save substantial time over the course of a week or month.
Mechanical intermittent drives can still be the right choice where production is stable and format variation is limited. They are often robust and economical. But when buyers compare prices without considering order mix, they risk choosing a lower-cost system that creates hidden labor and setup losses during everyday operation.
This is why procurement should ask suppliers to explain not just drive construction, but changeover logic. How many adjustments are manual. How long does format switching actually take under production conditions. Which parts require skilled operator intervention. These questions often reveal why intermittent motion drive price differs between competing machine offers.
How supplier scope changes the quoted price
Not every quotation covers the same scope. In practice, one supplier may price only the drive unit itself, while another includes motor sizing, controller integration, mounting assembly, commissioning support, operator training, spare parts recommendations, and warranty service. The second price will look higher, but the comparison is not equal.
Procurement teams should therefore separate component price from delivered system price. A drive that appears inexpensive can become costly once engineering adaptation, interface work, or startup troubleshooting is added. This is especially relevant in carton plants where uptime expectations are high and internal engineering resources may be limited.
Supplier reputation also affects price. Manufacturers with a proven installed base in packaging and converting sectors often charge more because they bring application-specific knowledge. They understand shock loads, board dust, register sensitivity, and line synchronization better than general industrial motion suppliers.
That premium is not always necessary, but it should be judged in relation to production risk. For mission-critical carton operations, support quality, spare part availability, and response speed may justify a higher upfront figure more than marginal hardware differences do.
How to compare intermittent motion drive price without making a false economy decision
The most effective procurement approach is to compare drives through total production value, not only through the purchase line item. Buyers should build a structured comparison around six factors: output stability, accuracy, changeover time, maintenance demand, energy use, and service support.
Start by matching the drive to the actual application. A plant running high-volume standard cartons does not need the same motion flexibility as a converter handling frequent design changes, retail packaging variation, or traceability-heavy pharmaceutical carton work. Over-specifying wastes capital, but under-specifying raises operating cost.
Then ask for evidence. Suppliers should be able to provide cycle ratings, reference installations, maintenance interval guidance, spare parts expectations, and integration details. If a vendor explains price only in broad terms, procurement should treat the quote with caution.
It is also useful to translate technical differences into production cost. For example, if a more expensive intermittent drive reduces setup time, prevents registration drift, or lowers stoppage frequency, buyers should estimate the annual value of those improvements. In many carton plants, the return becomes clear once labor, waste, and lost machine hours are included.
Energy efficiency should be considered, but in most cases it is not the primary price driver. More important are motion stability, durability, and fit with the production profile. Energy savings matter most where cycle frequency is high and the plant is already tracking power cost by equipment group.
When paying more makes sense and when it does not
Paying a higher intermittent motion drive price usually makes sense when the line runs at high speed, changes jobs frequently, requires tight registration, or supports premium carton quality where downtime and waste are expensive. In these conditions, better motion control often produces measurable operational return.
A higher price can also be justified when internal maintenance capacity is limited. If the drive supplier offers easier servicing, stronger diagnostics, and faster spare part support, the reduction in risk may outweigh the initial capital difference.
However, premium pricing is not always necessary. For stable product ranges, moderate speeds, and less complex formatting tasks, a simpler and proven mechanical intermittent drive may deliver the best value. Procurement should resist paying for digital flexibility that the plant will rarely use.
The right decision depends on production reality, not technology fashion. Buyers who connect drive specifications to order mix, machine utilization, labor conditions, and quality risk will make better investment choices than those who compare only headline prices.
Conclusion: the best price is the one that protects production value
In modern carton lines, intermittent motion drive price is shaped by far more than the hardware itself. The real drivers include torque performance, accuracy, speed stability, maintenance design, control integration, supplier support, and the operational demands of the converting process.
For procurement teams, the key lesson is clear. A low quotation may reduce upfront spending, but it can increase total cost through downtime, slower changeovers, weaker consistency, and higher maintenance demand. A higher quotation may be justified when it protects throughput, quality, and scheduling reliability.
The strongest buying decisions come from evaluating intermittent motion drives as production assets rather than catalog components. When buyers compare application fit, lifecycle cost, and supplier capability together, they are far more likely to choose a system that supports long-term carton plant performance instead of only short-term budget targets.
Related News
 How to Compare Folder Gluer Systems for High-Mix Carton ProductionCompare Folder Gluer Systems for high-mix carton production with practical insights on changeovers, accuracy, glue control, integration, and lifecycle support.Post-Press Kinematics Expert
 How Mechanical Gripper Systems Improve Repeatable Material HandlingMechanical gripper system solutions improve repeatable material handling, reduce waste and downtime, and protect products across fast-paced packaging and printing lines.Post-Press Kinematics Expert
 How a Die Cutter Gripper System Improves Sheet Control and AccuracyDiscover how a die cutter gripper system improves sheet control, registration accuracy, stripping consistency, and packaging production efficiency.Post-Press Kinematics Expert
 How to Select a Precision Cam Indexer for High-Speed AutomationSelect a precision cam indexer for high-speed automation with confidence. Learn how to evaluate inertia, dwell time, accuracy, loads, and maintenance needs.Post-Press Kinematics Expert
 Why Intermittent Motion Drive System Accuracy Matters in Die CuttingIntermittent motion drive system accuracy is critical in die cutting. Learn how it improves registration, reduces waste, and boosts carton quality and line efficiency.Post-Press Kinematics Expert
 What Shapes Intermittent Motion Drive Price in Modern Carton LinesIntermittent motion drive price depends on accuracy, durability, controls, and supplier scope. Discover how carton plants compare cost, uptime, and lifecycle value before buying.Post-Press Kinematics Expert