Common Carton Coding Problems and How to Fix Poor Print Readability
In carton coding, poor print readability usually shows up in the least convenient way: a box is already moving down the line, the code looks light or broken, and the next station flags it for rework. For maintenance teams, that is not just a print issue. It can slow down packing, interrupt traceability, and create avoidable waste when cartons have to be diverted or reworked by hand.
With carton coding machines, the problem often sits somewhere between the substrate, the ink delivery path, and the machine settings. The code may look fine on the machine screen but fail on the carton because the board surface is dusty, curved, absorbent, or moving slightly out of position. The good news is that most readability issues can be narrowed down with a practical sequence of checks instead of random parameter changes.
Start with the symptom, not the guess
When a printed code is hard to read, the first step is to describe the defect as precisely as possible. Is the text faint, blurred, missing strokes, smeared, or shifted off position? Each pattern points to a different source. A pale code often suggests weak ink transfer or poor contrast. Smearing usually means the ink is drying too slowly, the carton surface is too rough, or the printhead is too close. Gaps in characters may point to clogged nozzles, while uneven placement is often tied to timing or registration.
This matters because many teams try to “fix” everything at once. They change pressure, speed, and ink settings together, then lose track of which adjustment helped. A cleaner approach is to isolate one variable at a time and watch the printed result for a full run, not just one carton.
Readability problems that show up most often
On corrugated cartons and folded cases, the surface is rarely uniform. That means the same settings can behave differently from one job to the next. Common signs include:
- characters that fade on the flute peaks but appear darker in the valleys;
- broken barcode bars caused by weak drop placement or nozzle interruption;
- ink feathering into an uncoated board surface;
- codes that drift when the carton height or guide position changes;
- readability that gets worse after a machine stops and restarts.
Check the ink path before touching the settings
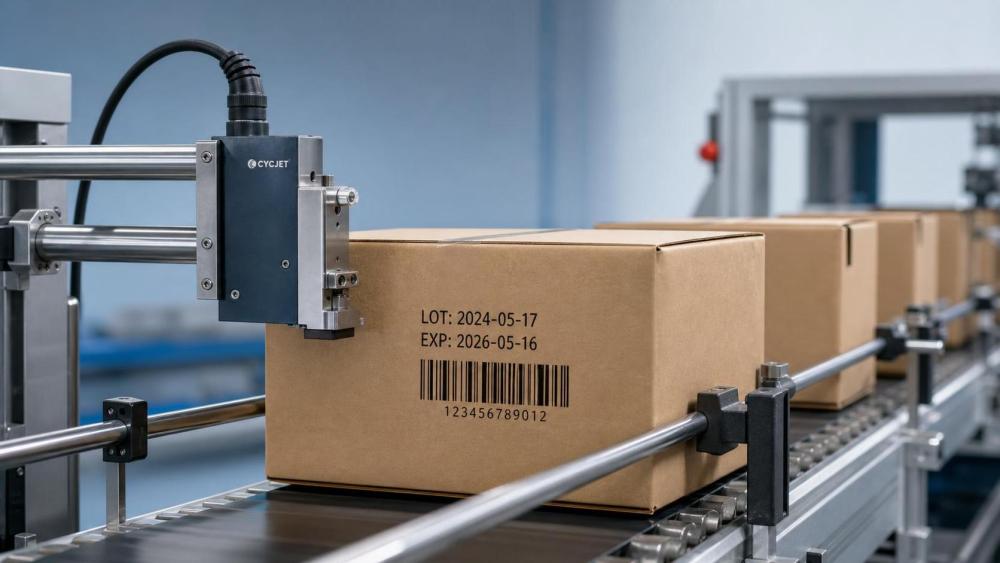
One of the most common mistakes is adjusting the machine before confirming that ink delivery is stable. If the system is starved, aerated, or partially blocked, no amount of timing correction will give a clean mark. Maintenance staff should first inspect the ink level, filter condition, tubing, and any signs of dried residue around the printhead area. If the print is inconsistent across repeated cartons, that often means the supply path is not steady enough.
For carton coding machines using CIJ or similar ink systems, nozzle condition matters just as much. A partially blocked nozzle can still print, but the character edges will look rough or incomplete. Cleaning routines should follow the machine’s recommended method, not a quick wipe that pushes debris deeper into the head.
Look at alignment and distance next
If the code is clear on one side and weak on the other, printhead position may be the issue. The distance between the head and the carton should stay within the practical range for the machine and substrate. Too far, and the drops spread or miss the target; too close, and contact or splash can distort the image. On uneven corrugated surfaces, a small deviation becomes visible quickly.
Alignment is not only vertical. Angle matters too. A slight tilt can affect barcodes more than text because barcode scanners need consistent bar width and spacing. If the line runs fast, check whether product guides, conveyors, or side rails are keeping each carton in the same position through the print zone. A good code on a test sample means little if the carton shifts under load during normal production.
Substrate variation can make a good setup look bad
Different cartons absorb ink differently, even when they look similar. Recycled board, coated board, and rough kraft surfaces all behave in their own way. When readability drops after a board change, it is often not a machine failure. The ink may need longer drying time, a different drop setting, or a small adjustment in print density. If the code looks sharp but rubs off, the issue may be drying rather than formation.
It helps to keep the code area clean and free of dust, adhesive mist, or fiber debris. A contaminated surface can break the ink film before it settles. When this happens, maintenance teams sometimes increase ink output to compensate, which can make smearing worse. A better habit is to confirm the substrate condition first, then tune the print only as much as needed.
Machine settings should support the line, not fight it
Speed, trigger timing, and character size all need to match the actual line behavior. If the carton spacing changes or the conveyor speed fluctuates, the code may appear shifted even though the printhead is functioning correctly. This is especially noticeable with carton coding machines used on mixed-format lines, where one setting has to serve several carton sizes.
When readability is unstable, review the trigger source and encoder input if the system uses one. A delayed trigger can place the code too near a fold or edge. If the text is too small for the chosen surface, increase the character height before increasing ink density. Bigger characters are often easier to read than darker ones, especially on textured board.
A simple correction path that usually saves time
- Confirm the defect type by looking at several cartons in a row.
- Inspect ink level, tubing, filters, and nozzle condition.
- Verify printhead distance, angle, and physical stability.
- Check carton surface quality and whether dust or moisture is present.
- Review timing, line speed, and character settings one at a time.
This sequence avoids the common trap of treating every poor print as a head failure. In practice, many readability complaints come from small mechanical or process shifts rather than a major part replacement.
When the issue keeps coming back
If the code becomes unreadable only after long runs, look for heat buildup, gradual nozzle drying, or a mounting point that loosens during vibration. If the problem returns after each restart, the startup purge or recovery routine may need attention. And if the defect appears on only one carton style, document the board type, print zone, and machine setup so the next changeover starts from a known baseline.
For teams maintaining high-speed packaging lines, a good rule is to treat print readability as a shared result of the machine, the substrate, and the line conditions. Once that is accepted, troubleshooting becomes more practical: verify the ink path, restore stable alignment, then tune the settings to the carton instead of forcing the carton to accept the same setting every time.
Most poor print readability problems can be reduced with steady inspection habits and small corrections made in the right order. That keeps the line moving, protects traceability, and helps avoid unnecessary rework when cartons are already packed and ready to go.
Related News
 Why Inkjet Printhead Prices Vary with Design and Ink CompatibilityCompare inkjet printhead price factors, from nozzle design to ink compatibility. Discover how to assess performance, reduce replacement risks, and choose better value for your printing system.Machine Vision & Coding Fellow
 How Inkjet Printheads Affect Code Quality and Maintenance CostsInkjet Printheads directly influence code clarity, barcode reliability, downtime, and maintenance costs. Learn practical steps to prevent defects and extend printhead life.Machine Vision & Coding Fellow
 How to Evaluate an OEM TIJ Printer Manufacturer for Production LinesChoose an OEM TIJ printer manufacturer with confidence: evaluate print quality, ink compatibility, integration, uptime, and total cost for reliable production-line coding.Machine Vision & Coding Fellow
 What Determines Inkjet Printhead Price in Industrial Coding SystemsInkjet printhead price depends on technology, ink compatibility, resolution, maintenance, and uptime. Learn how to compare total ownership cost and choose the right coding solution.Machine Vision & Coding Fellow
 How to Choose an Inkjet Printhead Supplier for Reliable ProductionChoose an inkjet printhead supplier with confidence. Learn how to verify compatibility, quality control, technical support, traceability, and total production cost.Machine Vision & Coding Fellow
 When Are Thermal Inkjet Printers the Right Choice for Product Coding?Thermal Inkjet Printers deliver crisp, flexible product coding for cartons, QR codes, barcodes, and variable data. Discover when TIJ is the right fit for your line.Machine Vision & Coding Fellow