



How Inspection Cameras Catch Inline Print Defects Before Shipment
A print job can look acceptable at press start and still develop defects later in the run. A slight registration drift, a weak barcode, a missing variable code, or a streak caused by ink buildup may affect only part of an order, yet that part can be enough to trigger rejection, rework, or a shipment hold. The risk is greatest when sheets, labels, cartons, or corrugated blanks move quickly through printing and converting with no reliable way to verify every unit.
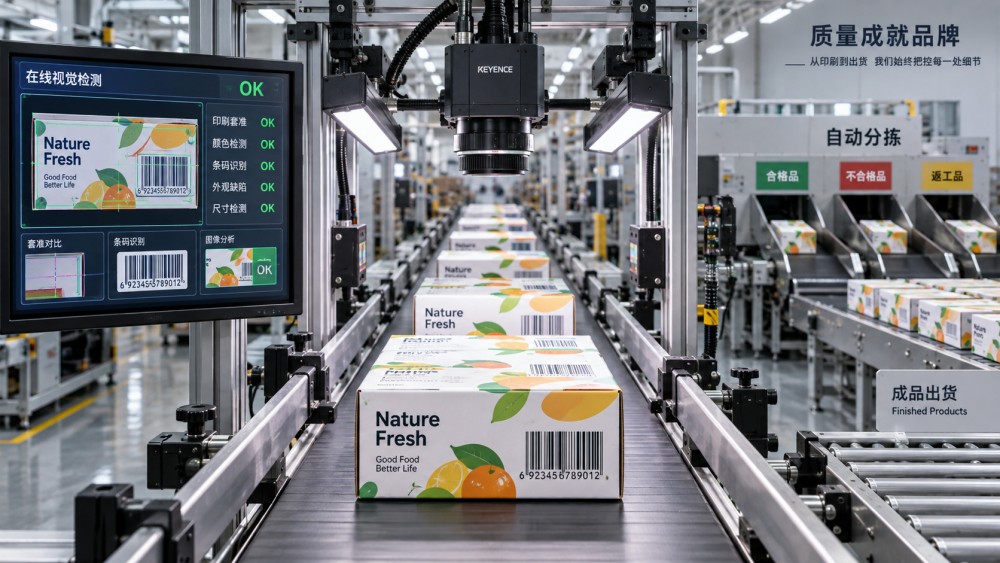
Inspection Cameras catch inline print defects before shipment by comparing each passing product against defined quality criteria in real time. Rather than relying on periodic visual samples, the system captures images during production, detects deviations in graphics, color zones, print position, codes, text, and surface appearance, and then sends an alarm, marks the defect, records the event, or triggers rejection according to the line setup. Their value is not simply “seeing” defects; it is creating a controlled response before questionable material reaches packing or dispatch.
Where shipment risk usually begins
Manual inspection is still useful, but it has natural limits. An operator may inspect the first sheets after setup, check samples at intervals, and review finished stacks before release. That approach can miss short-lived defects between sampling points. It can also struggle with subtle errors that become easier to see only when compared against a known reference image.
In commercial printing and packaging production, defects often emerge from conditions that change while the press is running:
- Web or sheet movement causes print-to-die-cut or color-to-color registration to shift.
- Ink density changes as viscosity, anilox transfer, doctor blade condition, drying, or press speed changes.
- A plate, blanket, sleeve, or print cylinder picks up debris and creates a repeating void or mark.
- Variable-data content is missing, duplicated, unreadable, or printed in the wrong location.
- Substrate variation, dust, coating differences, or board warp affects image appearance.
- Finishing stages introduce scuffing, foil placement errors, glue contamination, or damage to printed areas.
These are not always obvious at the delivery end. A defect may be visible only under consistent lighting, at full production speed, or after image magnification. By the time it is noticed in a packed pallet, the factory may need to quarantine a large quantity because the exact start and end of the defect are uncertain.
Inline vision changes this situation. Instead of asking, “Did the last sample look acceptable?” the production team can ask, “Which units failed, what type of failure occurred, and when did the condition begin?” That difference supports faster containment and a more defensible shipment-release decision.
What an inline camera system actually checks
Inspection Cameras are configured around the specific defect risks of a product and process. A camera alone does not guarantee meaningful inspection. The practical result depends on image resolution, lighting, product presentation, triggering accuracy, software logic, reference data, and how the line handles a detected fault.
For printed cartons, corrugated packaging, labels, inserts, and commercial print, the inspection task commonly falls into several categories.
A single line may require more than one inspection point. For example, a flexographic press may inspect print content immediately after the print stations, while a folder gluer may need a second check after folding and code application. A corrugated box plant may inspect printed board before die-cutting, then verify printed code position or finished carton condition later in the process. The right point is usually where the defect can still be corrected or isolated with the least material loss.
From camera image to a usable production decision
Inline inspection works best when its detection rules are connected to clear operating actions. A camera system can identify a deviation, but the factory must decide what happens next. Without that decision logic, operators may receive frequent alarms without knowing whether to stop the line, adjust the press, remove a limited number of sheets, or investigate a wider quality risk.
Establish the approved reference carefully
The inspection reference should represent the approved production condition, not merely the first acceptable sheet. It may be a master image, approved artwork file, golden sample, or a combination of print reference and variable-data rules. Areas that are intentionally variable must be defined as such. Otherwise, the system may flag valid differences as defects, creating unnecessary alarms.
The reference also needs sensible tolerances. Printed packaging is not a perfectly static object. Some movement, substrate texture, and minor tonal variation may be normal. Tolerances that are too wide allow genuine defects through; tolerances that are too tight can create nuisance rejects and reduce operator confidence. The goal is to distinguish acceptable production variation from a defect that affects use, traceability, appearance, or customer acceptance.
Set inspection zones according to risk
Not every part of a package carries equal importance. A small barcode, mandatory warning text, pharmaceutical lot code, or brand logo may require tighter controls than a large noncritical background area. Defining zones by risk helps the system focus on defects that matter most.
Typical zone decisions include:
- Use strict verification for barcodes, QR codes, serialized text, dates, lot numbers, and regulated product identifiers.
- Apply registration limits around fine text, borders, die-cut windows, and graphics that must align with a crease or cut line.
- Monitor large solids for streaks, print skips, contamination, and density change.
- Mask areas where substrate texture or intentional design variation would otherwise cause false alarms.
- Separate critical artwork elements from cosmetic areas so response urgency reflects actual risk.
This setup work is often where quality teams gain the most value. A generic “defect detected” message is less useful than a classification such as “barcode contrast below threshold,” “cyan registration shift,” or “missing text in inspection zone.” Clear categories make troubleshooting faster and improve the quality record.
How defects are caught early enough to prevent shipment problems
The main advantage of inline inspection is timing. Detection near the source of the defect limits the amount of affected material produced after the fault begins. However, early detection only becomes prevention when the workflow includes containment and verification.
- Detect the deviation. The system identifies a mismatch against the approved reference, a code-reading failure, an out-of-position feature, or a surface anomaly.
- Identify the product position. The event should be linked to a sheet count, web position, batch, job number, or other production identifier. This allows affected material to be located instead of treating the full run as suspect.
- Apply the planned response. Depending on severity, the line may reject the item automatically, mark it for removal, alert the operator, slow down, or stop. A missing batch code may justify immediate action, while a minor cosmetic trend may call for adjustment and increased observation.
- Correct the source condition. Operators inspect likely causes such as plate cleanliness, ink delivery, web tension, registration control, print pressure, curing, camera lens contamination, or product handling.
- Verify recovery. The line should not be assumed to be back in control merely because an adjustment was made. Inspection results must show that the defect has stopped and that the printed output again meets the defined limits.
- Contain material made during the event. Production records help define the interval from the last confirmed good unit to the first confirmed good unit after correction. That interval can then be re-inspected, removed, or otherwise handled under the plant’s quality procedure.
This sequence is especially important for intermittent defects. A repeating streak may be easy to see, but an occasional unreadable code or random void can appear only once every several hundred pieces. Periodic manual checks are least reliable in that situation. Continuous image capture gives the team evidence that the event occurred and shows whether it was isolated or recurring.
Choosing the right camera arrangement for the line
The best arrangement is driven by defect size, product speed, material movement, and the inspection task. A system designed to read large carton graphics does not necessarily have enough resolution to verify very small characters. Likewise, a high-resolution camera may be unsuitable if its image capture rate cannot keep pace with the line.
Before defining equipment requirements, map the product path. Determine whether the product is a continuous web, individual sheet, folded carton, or finished case. Check whether the surface is flat at the inspection point, whether it vibrates, and whether dust, glare, varnish, foil, or transparent film will affect image quality. Lighting needs equal attention. Glossy coatings can create reflections that hide a defect or create false contrast. Uneven ambient light can make a stable print appear to fluctuate.
Triggering must also be consistent. The camera needs to capture the same product position every cycle. Encoder-based triggering is often useful where speed varies, while fixed product sensors may be appropriate for discrete items. In either case, poor synchronization can look like a registration issue even when the printing itself is stable.
Do not confuse detection capability with rejection capability
A camera may detect a defective item without automatically removing it. On a sheet-fed line, the defective sheet may need to be marked and separated at delivery. On a web process, the system may record the location for later removal or activate a reject mechanism downstream. On a folder gluer, the reject station must respond fast enough to remove the exact carton identified by the inspection event.
Quality planning should therefore cover the full chain: camera detection, signal transfer, product tracking, reject timing, physical separation, and confirmation that rejected material cannot return to good stock. A well-configured inspection station with a weak reject process can still allow defective product to move into finished inventory.
False alarms are a process issue, not just a software issue
Teams sometimes disable sensitivity after repeated nuisance alarms. That can be understandable during a difficult job, but it creates a gap precisely when inspection is needed. Frequent false alarms should be treated as a setup or process investigation.
First, check the physical image conditions: lens cleanliness, lighting stability, camera mounting, vibration, trigger timing, and product presentation. Then review the reference image, tolerance settings, masked zones, and defect classification rules. Finally, determine whether the “false” event is actually showing a process variation that has not yet been defined as unacceptable. For example, recurring gloss variation may be harmless for one product but unacceptable for another where barcode readability or brand appearance is affected.
Operators also need a simple way to distinguish system status from product status. An alert caused by a blocked lens should not be handled the same way as an alert caused by missing legal text. Keeping equipment-health alerts separate from print-quality alarms avoids confusion and supports quicker action.
Making inspection records useful at shipment release
Inspection data is most valuable when it supports a practical release decision rather than becoming a large archive of images. Records should connect the job, production interval, defect category, response taken, and disposition of affected material. The level of detail depends on the product risk and internal quality requirements, but the purpose remains the same: prove that defects were detected, investigated, and contained before shipment.
For routine work, a useful review may include alarm frequency by defect type, periods when rejects increased, repeat events after an adjustment, and whether a specific press condition is linked to a defect trend. These observations can reveal issues that ordinary end-of-shift sampling may not show, such as a defect that begins after a particular running duration or appears only at higher speed.
Before dispatch, the release team should be able to answer a few direct questions: Was the approved reference used? Were critical codes and artwork zones inspected? Did any unresolved alarm intervals remain? Were rejected or suspect products physically segregated? Has the line demonstrated stable output after any corrective adjustment? When those answers are supported by production records, shipment approval becomes less dependent on assumption.
When inline inspection needs a broader process review
Some defects cannot be solved by camera settings alone. Persistent registration variation may indicate mechanical wear, unstable web tension, feeder inconsistency, or changing board dimensions. Repeated print voids may point to ink contamination, anilox condition, plate damage, pressure settings, or drying behavior. Low code readability can result from unsuitable ink, poor contrast, substrate absorption, print gain, or code design rather than a vision-system fault.
In these situations, Inspection Cameras still provide a useful starting point because they show the pattern, location, and recurrence of the problem. The next step is to connect that evidence with press settings, material batches, maintenance observations, and finishing conditions. The camera system acts as an early warning and verification layer; it does not replace disciplined process control.
Used this way, inline inspection prevents more than visibly defective print from leaving the factory. It gives production and quality teams a repeatable method to detect deviations as they occur, isolate affected output with greater precision, confirm that corrective action worked, and release shipments with stronger control over print quality and traceability.
Related News
 How to Select an Area Scan Camera for Reliable Print InspectionChoose an area scan camera for print inspection with confidence. Learn how resolution, lighting, speed, and testing affect defect detection—and make a smarter investment.Machine Vision & Coding Fellow
 How to Build a Reliable Compact Vision Sensor Inspection SystemBuild a reliable compact vision sensor inspection system with proven guidance on lighting, triggering, defect detection, and production-ready quality control.Machine Vision & Coding Fellow
 How High Accuracy Spectrophotometers Improve Print Color Controlhigh accuracy spectrophotometers help print and packaging teams detect color drift early, reduce waste, improve approvals, and protect brand consistency across every production run.Machine Vision & Coding Fellow
 How Spectrophotometers for Color Matching Improve Print ConsistencySpectrophotometers for color matching help printers control Delta E, reduce waste, and deliver reliable brand color across every press run.Machine Vision & Coding Fellow
 How Print Inspection Systems Prevent Defects Before ShipmentPrint Inspection Systems help detect print, barcode, color, and coding defects in real time—improving traceability, reducing waste, and preventing costly shipment failures.Machine Vision & Coding Fellow
 Smart Cameras for Inspection That Catch Print Defects in Real TimeSmart camera for inspection solutions catch print defects in real time, verify codes, reduce false rejects, and strengthen packaging quality control.Machine Vision & Coding Fellow





